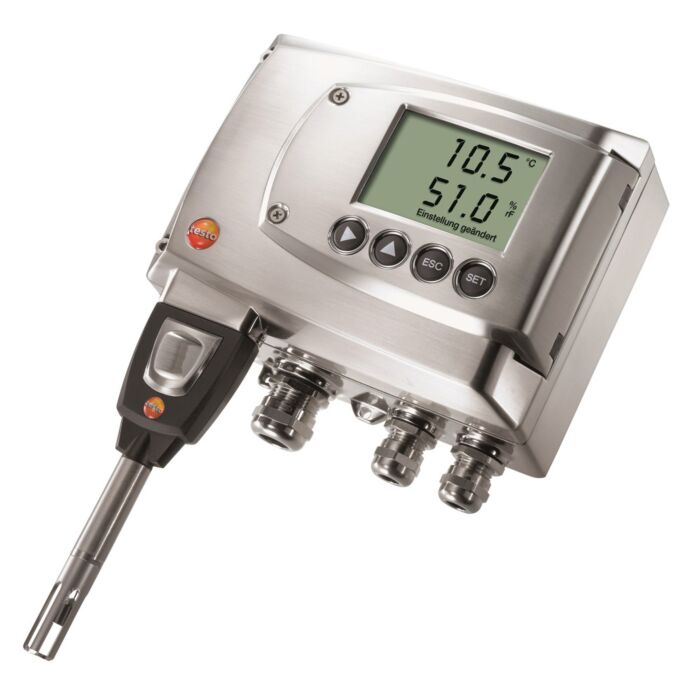
Industrial humidity measurement demands absolute professionalism. Not only in running the system, but also in the measuring technology used. The industrial humidity transmitter testo 6681, combined with the probe series testo 661x fulfils these high demands. The testo 6681 has a number of additional features, above and beyond the properties and benefits of a conventional transmitter, which will delight practitioners. This and other reasons make the testo 6681 the first choice in drying technology, trace humidity and compressed air process technology, as well as in demanding air conditioning technology, e.g. in cleanrooms.
- Optimum adjustment concept thanks to adjustability of the entire signal chain incl. analog adjustment
- Ethernet, relay and analog outputs allow optimum integration into individual automation systems
- Self-monitoring and early warning guarantee high system availability
- Calculation and presentation of all relevant humidity parameters
- P2A software for parameterization, adjustment and analysis saves time and costs in commissioning and maintenance
- Display with multi-language display
- Robust, easy-to-clean metal housing
Applications
- Drying Processes
- Cleanrooms & Test Benches
- Food Production
- Sterilization & H2O2 Environments
- Trace Humidity & Compressed Air Technology
- Painting & Coating Installations
- Bio-Research & Laboratories
- Museums & Archives
- Electronics & Storage
Each Unit Includes
- Industrial Temperature/ humidity transmitter (0555 6681)